8011 aluminum foil anneal
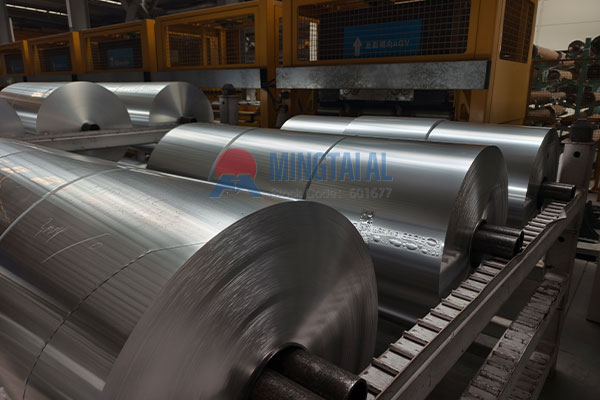
8011 aluminum foil anneal addresses two common issues in foil that has been cold rolled to final gauge. In H18 temper, the surface carries residual rolling oil, while the internal structure holds accumulated processing stress. During later lamination, slitting, or forming, oil marks can weaken adhesion, and a hard, brittle foil may crack. The key questions are how to remove the oil and how to soften the foil. Annealing must solve both at the same time.
Annealing serves three main purposes:
- Removes residual rolling oil from the surface.
- Relieves internal processing stress.
- Produces a soft, uniform O temper.
How Degreasing and Softening Happen Together
Degreasing
When the coil is heated, rolling oil vaporizes and escapes through the gaps between foil layers toward the coil edges. If the temperature rises too quickly, the oil cannot escape in time and may form carbonized oil marks. If it rises too slowly, efficiency drops. Temperature and heating rate together determine surface cleanliness.
Softening
Recrystallization allows deformed grains to nucleate and grow again. Dislocations decrease, and processing stress is released. The foil changes from H18 temper to O temper, with higher elongation and better flexibility.
Degreasing and softening occur in the same annealing cycle. The key is to keep the two processes from interfering with each other.
Key Process Parameters
Annealing results cannot be judged by temperature alone. Several factors should be reviewed together:
- Temperature uniformity: Large temperature differences across the coil can cause uneven softness.
- Soaking sufficiency: Both the center and the edges need complete recrystallization.
- Heating and cooling rates: These affect oil drainage, grain size, and residual stress.
- Furnace atmosphere: Nitrogen protection helps reduce oxidation and water-stain defects.
- Furnace loading: Coil diameter, coil weight, and interlayer tension all affect heat transfer.
These parameters must match the alloy temper, thickness, and final application. There is no universal parameter set.
How to Judge Quality After Annealing
Surface cleanliness: In a wipe test or wetting test, the surface should wet evenly with no clear oil marks.
Mechanical properties: O temper should be soft, with enough elongation for later forming. If it remains hard, recrystallization is incomplete.
Pinhole count: Grain coarsening or trapped gas can increase pinholes and affect barrier performance.
Unwinding performance: There should be no interlayer blocking, and unwinding tension should remain stable.
Together, these indicators show whether annealing is acceptable.
What Annealing Can and Cannot Solve
Annealing mainly removes residual rolling oil and processing stress. If oil marks are severe or the oil is difficult to vaporize, annealing alone may not remove them completely. Annealing is also part of the production process. It does not involve surface treatment or further processing. When hydrophilic, corrosion-resistant, or coating functions are needed, they must be added in a later step.
Thickness uniformity and coiling quality of the upstream cold-rolled coil also affect annealing results. Stable annealing starts with stable incoming cold-rolled material.
FAQ
Q: Is a slight oily feel normal after annealing 8011 aluminum foil?
A: A slight feel may come from the oxide film, but clear oil marks or uneven wetting usually mean degreasing is incomplete.
Q: What is the main difference between O temper and H18 temper?
A: O temper is fully annealed, soft, and has high elongation; H18 temper is stronger but harder and more brittle.
Q: Can annealing replace surface treatment?
A: No. Annealing only removes oil and softens the foil; it does not change surface function.
For 8011 aluminum foil anneal, Henan Mingtai Aluminum supplies 8011 aluminum foil with stable annealing control. The O temper product offers clean surfaces and uniform softness for pharmaceutical packaging, food lamination, and similar applications. For a specification sheet or sample, please contact us.