aluminum coil width tolerance standard
An aluminum coil width tolerance standard defines the acceptable range for slit coil width, but it does not decide what your production line can actually handle. A coil can pass inspection and still cause stamping burrs, welding misalignment, or roll forming drift. The issue is often not the equipment—it is a mismatch between the specified tolerance and the downstream process.
This is why width tolerance deserves more attention at the ordering stage, not after the coil is on the machine.
Tighter Is Not Always Better
Standards usually divide width tolerance into standard and high-precision grades. Standard grade covers general use. High-precision grade serves demanding lines. Choose too tight, and cost rises. Choose too loose, and the line suffers. The right choice depends on how the coil will be used.
A practical approach: first confirm how much width variation your line can accept, then work backward to the needed grade. If you are unsure, start with a small trial slit coil before committing to a full order.
Common Standard Systems
Different markets refer to different standards:
- GB/T 3880.3 (China): specifies width deviation for cold-rolled aluminum strip, with standard and high-precision grades.
- EN 485-4 (Europe): applies to cold-rolled aluminum strip and covers width, camber, and other shape tolerances.
- ISO 6361-3 (International): applies to cold-rolled aluminum strip and also defines width and lateral curvature tolerances.
These standards give allowable ranges, not application advice. Exporting to Europe, domestic industrial applications, or a cross-border project may point to different systems. Higher grades demand more from slitting equipment, master coil flatness, and inspection. That is where price differences often come from.
Why Width Can Shift After Slitting
Master coil flatness is the foundation. If the master coil has edge waves or camber, slitting cannot fully remove them.
Tool condition and tension control matter just as much. Incorrect knife clearance can affect both width and burrs. Unstable tension can make the strip drift sideways, causing head-to-tail width variation. Coil winding alignment also affects end face quality and later feeding.
These factors are not written into the standard, but they decide real performance. This is why two suppliers can both quote “high-precision” and still deliver very different coils.
Match Tolerance to the Application
- High-frequency welded tube: Width must be stable so overlap does not vary. A tighter tolerance grade is usually recommended.
- Stamping: Look at die clearance. Normal automatic feeding and high-speed precision stamping tolerate width variation very differently.
- Architectural roll forming: Width can be more relaxed, but camber must be controlled, or edges will not align after forming.
- Battery and new energy applications: Some applications require very tight width control. Say so at the inquiry stage and confirm whether the line and inspection method can match.
So instead of asking only “What is the standard?” ask “How much width variation can my line accept?” If unsure, a small trial run can help set the right tolerance before mass production.
What to Confirm Before Ordering
1. Nominal width and tolerance direction: Is it bilateral or unilateral? Put it in writing.
2. Tolerance grade: State a specific value, not just “according to standard.”
3. Edge condition: How much burr is acceptable? Does the edge need special handling?
4. Coil consistency: Can head, middle, and tail width data be provided?
5. Master coil source: Flatness directly affects slitting results.
6. Packaging and transport: Edge damage can affect unwinding. Agree on protection if needed.
Clear these points before shipment, and you avoid the argument that the coil is “within size but not usable.” A short technical agreement covering specification, inspection, and acceptance criteria can save time later.
A Note from Mingtai Al.
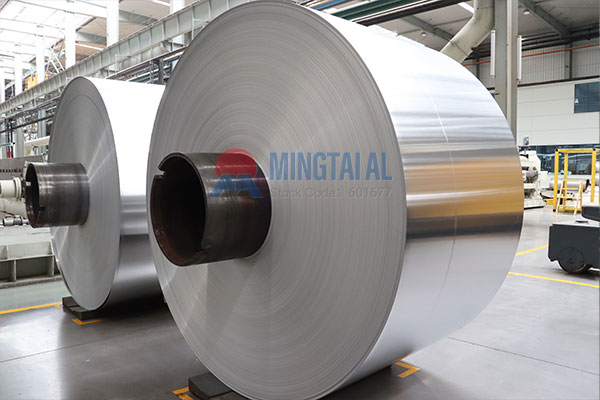
Henan Mingtai Al. supplies base aluminum coils with precision slitting and width customization. We do not provide surface treatment or further processing. If you need help applying an aluminum coil width tolerance standard to your process, our technical team can suggest a suitable tolerance grade based on your downstream application.
FAQ
Q: How do I choose width tolerance for slit aluminum coil?
A: First check how much width variation your line can accept, then choose standard or high-precision grade.
Q: Is width tolerance more important than thickness tolerance?
A: In stamping, tube welding, and roll forming, width tolerance often affects die fit and weld overlap more directly.
Q: Can I request a tighter tolerance than the standard grade?
A: Yes, but price and lead time may change, so confirm the supplier’s line capability first.
Q: Which standards cover aluminum coil width tolerance?
A: GB/T 3880.3, EN 485-4, and ISO 6361-3 are the most commonly referenced.
Q: Does Mingtai provide surface treatment or further processing?
A: No. Mingtai supplies base aluminum coils with slitting and width customization only.